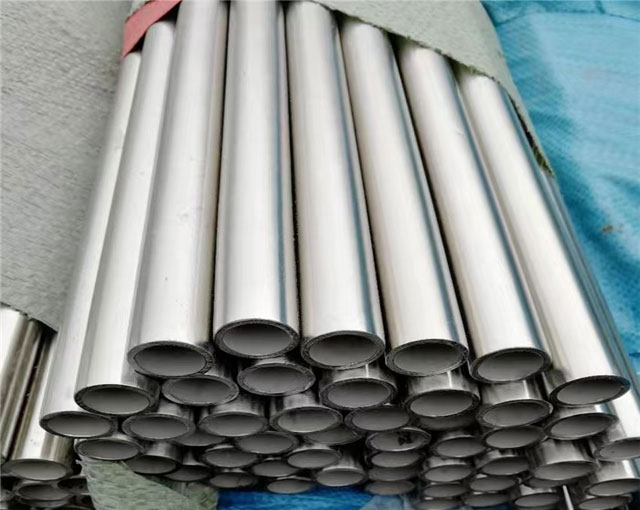
ASTM A790 Duplex Steel UNS S31803 Seamless Pipe
Premier Industrial Manufacturer, Supplier & Stockist of High-Strength Alloy 2205 (1.4462) Ferritic/Austenitic Dual-Phase Seamless Pipes for Corrosion-Critical Processing Environment
Werkstoff: 1.4462
PREN: 32 – 35
Executive Technical Summary: ASTM A790 UNS S31803
ASTM A790 UNS S31803 (commonly designated as Duplex Alloy 2205) is a nitrogen-enhanced, dual-phase ferritic-austenitic stainless steel engineered for application environments demanding elevated mechanical performance and localized corrosion defense. Incorporating an approximate 50/50 balance of austenite and ferrite phases, UNS S31803 seamlessly integrates the stress-corrosion cracking immunity inherent in ferritic alloys with the superior ductility, toughness, and pitting resistance typical of austenitic grades. Seamless pipes produced under ASTM A790 specifications undergo solid billet piercing, hot extrusion/cold drawing, and solution annealing to satisfy strict structural and dimensional criteria.
1. International Material Equivalent Standards
Comprehensive cross-reference table mapping UNS S31803 across international standardization organizations.
| Standard System | Grade Designation | UNS Number | EN / DIN Werkstoff Nr. | AFNOR / GOST | JIS Code |
|---|---|---|---|---|---|
| ASTM / ASME | Duplex 2205 | UNS S31803 | 1.4462 | Z3 CrNi 22.05 AZ | SUS 329J3L |
| ASTM / ASME (Dual) | Duplex 2205 Opt. | UNS S32205 | 1.4462 (X2CrNiMoN22-5-3) | 05Kh22N5M3T | SUS 329J4L |
| GB (China) | 022Cr22Ni5Mo3N | S22253 | — | — | — |
| ISO | X2CrNiMoN22-5-3 | — | 4462-318-03-I | — | — |
2. Chemical Composition Standard (ASTM A790 UNS S31803 vs S32205)
Elemental percentage limits per ASTM A790/A790M specifications (Weight % values).
| Grade | Carbon (C) | Manganese (Mn) | Silicon (Si) | Phosphorus (P) | Sulfur (S) | Chromium (Cr) | Nickel (Ni) | Molybdenum (Mo) | Nitrogen (N) | Iron (Fe) |
|---|---|---|---|---|---|---|---|---|---|---|
| UNS S31803 | ≤ 0.030 | ≤ 2.00 | ≤ 1.00 | ≤ 0.030 | ≤ 0.020 | 21.0 – 23.0 | 4.50 – 6.50 | 2.50 – 3.50 | 0.08 – 0.20 | Balance |
| UNS S32205 | ≤ 0.030 | ≤ 2.00 | ≤ 1.00 | ≤ 0.030 | ≤ 0.020 | 22.0 – 23.0 | 4.50 – 6.50 | 3.00 – 3.50 | 0.14 – 0.20 | Balance |
3. Mechanical and Physical Performance Limits
Minimum required values for room-temperature mechanical testing per ASTM A790.
| Property Parameter | Metric Unit (SI) | Imperial Unit | UNS S31803 Value |
|---|---|---|---|
| Tensile Strength, Min | 620 MPa | 90 ksi (90,000 PSI) | 620 – 880 MPa |
| Yield Strength (0.2% Offset), Min | 450 MPa | 65 ksi (65,000 PSI) | ≥ 450 MPa |
| Elongation in 2 in. (50mm), Min | 25 % | 25 % | 25 % |
| Hardness (Brinell / Rockwell C) | 290 HBW Max | 31 HRC Max | ≤ 290 HBW / 31 HRC |
| Modulus of Elasticity | 200 GPa | 29 x 10^6 psi | 200 GPa |
| Charpy V-Notch Impact Energy (-40°C) | ≥ 80 J | ≥ 59 ft-lbs | ≥ 80 J (Longitudinal) |
4. Seamless Pipe Manufacturing & Heat Treatment Steps
Inspection of raw round solid billets with full heat code tracking and PMI testing prior to processing.
Heating billets to 1150°C-1250°C followed by rotary piercing to transform solid bars into hollow shells.
Precision cold drawing or cold pilgering processes to reach tight wall thickness and outer diameter tolerances.
Heating to 1020°C–1100°C followed by immediate water quenching to prevent sigma phase precipitation.
5. ASME B36.19M / B36.10M Pipe Schedule Dimensions & Weights
Standard nominal pipe sizes (NPS), outer diameters, schedule wall thicknesses, and theoretical linear weights (kg/m).
| NPS (Inches) | DN (mm) | OD (mm) | SCH 10S WT (mm) / Wt | SCH 40S WT (mm) / Wt | SCH 80S WT (mm) / Wt | SCH 160 WT (mm) / Wt |
|---|---|---|---|---|---|---|
| 1/2″ | DN15 | 21.3 mm | 2.11 mm (1.02 kg/m) | 2.77 mm (1.29 kg/m) | 3.73 mm (1.64 kg/m) | 4.78 mm (1.98 kg/m) |
| 3/4″ | DN20 | 26.7 mm | 2.11 mm (1.30 kg/m) | 2.87 mm (1.71 kg/m) | 3.91 mm (2.23 kg/m) | 5.56 mm (2.94 kg/m) |
| 1″ | DN25 | 33.4 mm | 2.77 mm (2.12 kg/m) | 3.38 mm (2.54 kg/m) | 4.55 mm (3.29 kg/m) | 6.35 mm (4.30 kg/m) |
| 1-1/2″ | DN40 | 48.3 mm | 2.77 mm (3.16 kg/m) | 3.68 mm (4.11 kg/m) | 5.08 mm (5.50 kg/m) | 7.14 mm (7.36 kg/m) |
| 2″ | DN50 | 60.3 mm | 2.77 mm (3.99 kg/m) | 3.91 mm (5.52 kg/m) | 5.54 mm (7.60 kg/m) | 8.74 mm (11.28 kg/m) |
| 3″ | DN80 | 88.9 mm | 3.05 mm (6.56 kg/m) | 5.49 mm (11.47 kg/m) | 7.62 mm (15.51 kg/m) | 11.13 mm (21.68 kg/m) |
| 4″ | DN100 | 114.3 mm | 3.05 mm (8.50 kg/m) | 6.02 mm (16.32 kg/m) | 8.56 mm (22.67 kg/m) | 13.49 mm (34.06 kg/m) |
| 6″ | DN150 | 168.3 mm | 3.40 mm (14.04 kg/m) | 7.11 mm (28.30 kg/m) | 10.97 mm (43.21 kg/m) | 18.26 mm (68.60 kg/m) |
| 8″ | DN200 | 219.1 mm | 3.76 mm (20.28 kg/m) | 8.18 mm (43.20 kg/m) | 12.70 mm (65.63 kg/m) | 22.23 mm (109.67 kg/m) |
6. Permissible Variations in Dimensions (ASTM A999 / A790)
Permissible manufacturing variations in wall thickness, outer diameter, and cut lengths.
| Parameter | NPS Range | Over Tolerance | Under Tolerance |
|---|---|---|---|
| Outer Diameter (OD) | 1/8″ to 1-1/2″ (10.3mm – 48.3mm) | +0.4 mm (+1/64 in) | -0.8 mm (-1/32 in) |
| Over 1-1/2″ to 4″ (48.3mm – 114.3mm) | +0.8 mm (+1/32 in) | -0.8 mm (-1/32 in) | |
| Over 4″ to 8″ (114.3mm – 219.1mm) | +1.6 mm (+1/16 in) | -0.8 mm (-1/32 in) | |
| Wall Thickness (WT) | All Seamless NPS Ranges | +12.5 % nominal WT | -12.5 % nominal WT |
| Hydrostatic Test Pressure | All Sizes | P = 2St/D (Max 19.3 MPa / 2800 psi per ASTM A999) | |
7. Structural Comparison: UNS S31803 Seamless vs. Welded Pipe
Technical evaluation matrix for engineering selection based on manufacturing methodologies.
| Evaluation Criteria | ASTM A790 UNS S31803 Seamless Pipe | ASTM A790 UNS S31803 Welded Pipe |
|---|---|---|
| Starting Material | Solid Round Billets / Bars | Hot-rolled Plate / Coils |
| Weld Seam Integrity | 100% Homogenous (No Weld Joint) | Longitudinal Weld Joint Present (Joint factor 0.85 – 1.0) |
| Pressure Class Efficiency | Higher Working Pressure Rating | Standard Pressure Rating |
| Grain Boundary Consistency | Uniform Ferrite-Austenite Microstructure | HAZ (Heat Affected Zone) Requires Strict Annealing Control |
| NDT Inspection Standard | 100% UT (Ultrasonic) or Hydrostatic | 100% Radiographic Testing (RT) on Weld Seam |
| Available Size Range | NPS 1/2″ to 24″ (Extruded/Drawn) | NPS 6″ to 72″ (EFW/SAW) |
8. Pitting & Crevice Corrosion Performance (PREN Matrix)
Comparative Pitting Resistance Equivalent Number calculation: $\text{PREN} = \% \text{Cr} + 3.3 \times \% \text{Mo} + 16 \times \% \text{N}$.
| Stainless Grade | Alloy Structure | Typical PREN Range | Critical Pitting Temp (CPT) | SCC Chloride Resistance |
|---|---|---|---|---|
| AISI 304L | Austenitic | 18.0 – 20.0 | 10 °C | Poor (< 60°C) |
| AISI 316L | Austenitic | 23.0 – 25.0 | 15 °C | Moderate (< 60°C) |
| Duplex UNS S31803 | Duplex 50/50 | 32.0 – 35.0 | 35 °C | Excellent (> 150°C) |
| Duplex UNS S32205 | Duplex 50/50 | 35.0 – 38.0 | 38 °C | Excellent (> 150°C) |
| Super Duplex S32750 | Super Duplex | 42.0 – 45.0 | 65 °C | Outstanding |
9. Thermal Properties & Solution Treatment Specification
Physical thermal limits and full solution annealing process requirements per ASTM A790.
| Thermal Process / Metric | Required Parameter | Cooling / Medium Specification |
|---|---|---|
| Solution Annealing Temperature | 1020 °C to 1100 °C (1870 °F to 2010 °F) | Rapid liquid quenching (water) below 260°C |
| Melting Point Range | 1420 °C to 1465 °C (2588 °F to 2669 °F) | Base metal thermodynamic state |
| Thermal Conductivity (20°C) | 15 W/m·K | Measured across solution-annealed bar |
| Specific Heat Capacity (20°C) | 500 J/kg·K | Standard ambient thermal constant |
| Mean Coefficient of Thermal Expansion | 13.5 x 10^-6 / K (20°C to 100°C) | Lower expansion rate than 300 series austenitic |
10. Mandatory Factory Inspection & Quality Testing Protocol
Testing protocols executed to ensure 100% compliance with EN 10204 3.1 / 3.2 certification.
| Test Category | Standard Reference | Acceptance Criteria / Objective |
|---|---|---|
| Hydrostatic Pressure Test | ASTM A999 / A790 | No leakage at maximum calculated fiber stress for minimum 5 seconds. |
| Ultrasonic Testing (UT) | ASTM E213 | 100% volumetric inspection for internal cracks, voids, and inclusions. |
| Eddy Current Testing (ET) | ASTM E426 | Non-destructive detection of surface and sub-surface longitudinal defects. |
| Intergranular Corrosion (IGC) | ASTM A262 Practice E / ASTM G48 Method A | Verification of immunity to intergranular attack and pitting at 25°C/50°C. |
| Microstructure Ferrite Count | ASTM E562 / E1245 | Ferrite phase content maintained strictly within 40% to 60%. |
| Positive Material Identification (PMI) | XRF / OES Analysis | 100% verification of Cr, Ni, Mo, and N alloying elemental distribution. |
11. Industrial Sector Application Matrix
Deployment environments and specific use cases for ASTM A790 S31803 seamless piping systems.
| Industry Sector | Operating Sub-Systems | Key Operating Stress Factors |
|---|---|---|
| Oil & Gas Upstream/Offshore | Subsea flowlines, manifold piping, sour gas extraction, risers | High H2S, high CO2, chloride pitting, extreme pressure |
| Chemical Processing | Nitric acid production, organic acid vessels, heat exchangers | Aggressive acidic media, thermal stress, crevice corrosion |
| Desalination & Marine | Reverse osmosis (RO) high-pressure piping, seawater pumps | Ultra-high chloride concentrations, high fluid velocity, erosion |
| Pulp & Paper Manufacturing | Digesters, bleaching plant washers, liquor recovery systems | Chlorine bleaching agent attack, elevated temperatures |
| Petrochemical Refining | Hydrocracker process lines, distillation columns, reboilers | Hydrocarbon-chloride mixes, high tensile mechanical loads |
13. Welding Consumables & Fabrication Parameters
Recommended filler metals and interpass temperature controls for maintaining phase balance during welding.
| Welding Process | AWS Filler Classification | Shielding / Backing Gas | Max Interpass Temp |
|---|---|---|---|
| GTAW (TIG) | ER2209 | Pure Ar or Ar + 2% N2 (99.99%) | 150 °C (300 °F) |
| GMAW (MIG) | ER2209 | Ar + 1-2% O2 / Ar + He mix | 150 °C (300 °F) |
| SMAW (Stick) | E2209-15 / E2209-16 / E2209-17 | N/A (Coated Electrode) | 150 °C (300 °F) |
| SAW (Submerged Arc) | ER2209 + Basic Flux | Granular Basic Flux | 150 °C (300 °F) |
14. Quality Certification & Mill Documentation Package
Every order of ASTM A790 UNS S31803 seamless pipe is supplied with full material traceability records.
Certified Mill Test Certificates including heat chemistry, mechanical, and hydrostatic results.
Full compliance certification for sour oilfield service environments.
Inspection reports available by SGS, TÜV, Bureau Veritas, or Lloyd’s Register.
Complete verification of raw material heat numbers and original steel mill origin certificates.
15. Export Packaging & Surface Treatment Specifications
Standard surface finishes and seaworthy packaging types for international shipping.
| Packaging Element | Standard Options | Protection Objective |
|---|---|---|
| Surface Condition | Solution Annealed & Pickled (White Passivated) / Mechanically Polished | Restoration of passive chromium oxide layer; removal of surface scale. |
| Pipe End Treatment | Plain Ends (PE) / Bevelled Ends (BW 37.5°) per ASME B16.25 | Protection of end faces with plastic bevel protectors/end caps. |
| Seaworthy Containerizing | Hexagonal Bundles strapped with steel strips / Fumigated Wooden Cases | Prevents physical deformation, marine humidity exposure, and surface scratching. |
16. Technical Frequently Asked Questions (FAQ)
A: S32205 is a dual-certified, higher-chromium and higher-nitrogen strain of S31803. It guarantees higher corrosion resistance (higher PREN values) and tighter elemental control bounds, meeting both UNS S31803 and S32205 specifications simultaneously.
A: Seamless ASTM A790 pipe features a completely uniform dual-phase grain structure throughout its circumference. This eliminates the risk of preferential corrosion attacks along weld heat-affected zones (HAZ) and offers superior pressure ratings in critical subsea or high-pressure processing lines.
Request Technical Quote & Stock List
As a direct factory manufacturer of ASTM A790 UNS S31803 / S32205 seamless pipes, we maintain an extensive inventory from 1/2″ to 16″ in all schedules. Contact our technical sales engineering office for project inquiries, mill test certificates, and immediate price quotes.
Download Catalog

You must be logged in to post a comment.