Technical Metrics & Material Attributes
Its yield strength is substantially higher than that of common austenitic grades such as 316L.
The higher proof stress can allow thinner wall schedules where the design calculation permits.
The PREN value is commonly used to assess resistance to localized pitting and crevice corrosion.
Commonly selected for sour service, offshore systems, and demanding chemical-service piping.
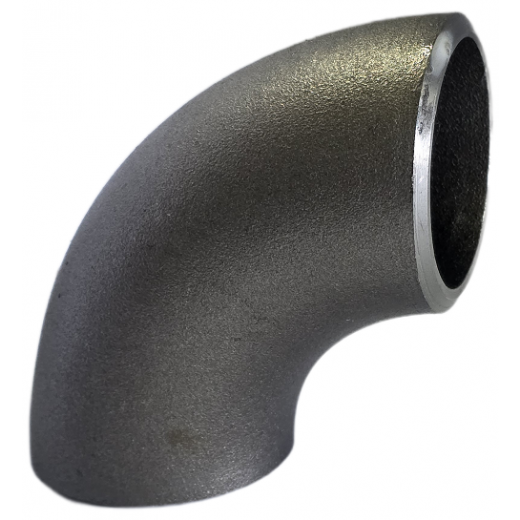
Material Overview: ASTM A815 WPS UNS S32750 Super Duplex-Winkelstücke
ASTM A815 WPS UNS S32750 is a wrought ferritic/austenitic super duplex stainless steel fitting grade used where strength and corrosion resistance are both important. It is used in marine, Petrochemie, Untersee, and chemical-processing service where conventional stainless steels may not provide enough margin, UNS S32750 (allgemein bekannt als 2507 Super Duplex oder EN 1.4410) bietet eine ausgewogene 50/50 Zweiphasiges Gefüge bestehend aus etwa gleichen Anteilen Austenit und Ferrit. The duplex structure combines relatively high yield strength with good resistance to chloride-related stress corrosion cracking (SCC), while retaining useful toughness when the phase balance is properly controlled.
Die Bezeichnung WPS in ASTM A815 weist auf nahtlose Rohrverbindungsstücke in Schmiedequalität hin, die gemäß den strengen Anforderungen von ASME B16.9 und MSS SP-43 hergestellt wurden. Diese Ellbogen, in beiden Varianten erhältlich Lange Radius (LR, R=1,5 D) und Kurze Radien (SR, R=1.0 D) Konfigurationen, are used to change flow direction in high-pressure piping networks. Ob in Tiefsee-Offshore-Bohrinseln eingesetzt, Umkehrosmose-Meerwasserentsalzungsanlagen, aggressive Sauergaswäscher, oder hochreine chemische Reaktoren, ASTM A815 WPS UNS S32750 elbows are intended for service involving cyclic loading, temperature changes, and corrosive process fluids.
Wichtige Materialklassifizierungen, die von der Spezifikation ASTM A815 abgedeckt werden:
- Klasse WP-S: Nahtlose Formstücke aus nahtlosem Rohr, Rohr, oder Schmiedematerial.
- Klasse WP-W: Geschmiedete Formstücke mit Schweißnähten, bei denen das Füllmetall hinzugefügt und zerstörungsfrei mittels Röntgen untersucht wurde (RT).
- Klasse WP-WX: Geschmiedete, geschweißte Beschläge, bei denen alle Schweißnähte vorhanden sind 100% radiographiert gemäß ASME Boiler and Pressure Vessel Code.
- Klasse WP-WU: Geschmiedete Beschläge, bei denen alle Schweißnähte vorhanden sind 100% mittels Ultraschallprüfung untersucht (OUT).
Grenzwerte für die chemische Zusammensetzung (%) – UNS S32750 vs. Duplex-Familie
Elemental limits are controlled to support corrosion resistance and to reduce the risk of undesirable intermetallic phases such as sigma (A) and chi (H).
| Klasse / UNS | KOHLENSTOFF (C) | Cr | Ni | Mo | n | Cu | MN (max) | Si (max) | P / S (max) |
|---|---|---|---|---|---|---|---|---|---|
| WPS S32750 (2507) | ≤ 0.030 | 24.0 – 26.0 | 6.0 – 8.0 | 3.0 – 5.0 | 0.24 – 0.32 | ≤ 0.50 | 1.20 | 0.80 | 0.035 / 0.020 |
| WPS S31803 (2205) | ≤ 0.030 | 21.0 – 23.0 | 4.5 – 6.5 | 2.5 – 3.5 | 0.08 – 0.20 | - | 2.00 | 1.00 | 0.030 / 0.020 |
| WPS S32202 (2202) | ≤ 0.030 | 21.5 – 24.0 | 1.0 – 2.8 | 0.45 max | 0.18 – 0.26 | - | 2.00 | 1.00 | 0.040 / 0.010 |
| WPS S32760 (null 100) | ≤ 0.030 | 24.0 – 26.0 | 6.0 – 8.0 | 3.0 – 4.0 | 0.20 – 0.30 | 0.50 – 1.00 | 1.00 | 1.00 | 0.030 / 0.010 |
* Hinweis: UNS S32750 enthält absichtliche Zusätze von Stickstoff (0.24–0,32 %) um die Lochfraßbeständigkeit deutlich zu erhöhen, fördern eine schnelle interkristalline Reaustenitisierung während der Wärmebehandlung, und erhöhen die mechanische Streckgrenze.
Mechanische & Strukturelle Leistungsdaten
The ferrite-austenite balance gives S32750 high tensile and yield strength, useful low-temperature toughness, and good resistance to erosion-corrosion. Im Vergleich zum Standard 300 Serienedelstahl oder konventionelle Lean-Duplex-Legierungen, Mit S32750 können Ingenieure Pläne für dünnere Wände festlegen (z.B., SCH 10S vs. SCH 40S) ohne Einbußen bei den strukturellen Sicherheitsmargen.
Where permitted by the applicable ASME B31.3 design conditions, the higher allowable stress can reduce required wall thickness and system weight.
ASTM A815 S32750 Mechanische Grenzwerte
| Mechanischer Parameter | ASTM A815 Standardgrenzwert |
|---|---|
| Zugfestigkeit, min (MPA / Ksi) | 800 – 965 / [116 – 140] |
| Streckgrenze (0.2% ausgleichen), min | 550 MPA / [80 Ksi] |
| Dehnung ein 2 in. (50 mm), min % | 15.0 % |
| Härte, Brinell (HBW), max | 310 HBW max |
| Härte, Rockwell C (HRC), max | 32 HRC max |
| Charpy V-Notch Impact Energy (-40° C) | ≥ 80 Joule (Durchschnittliche) |
Korrosionsbeständigkeitsphysik & PREN-Formelberechnungen
Pitting and crevice-corrosion resistance of Super Duplex UNS S32750 is commonly discussed using the Lochfraßfestigkeit Äquivalente Zahl (HOLZ). A higher PREN generally indicates greater resistance to localized passive-film breakdown in chloride-containing service.
Lochfraß & Spaltkorrosion
Mit einem Mindest-PREN von 42, S32750 elbows are generally selected for chlorinated seawater service when the temperature and chloride exposure are within the design limits.
Spannungsrisskorrosion (SCC)
Compared with many austenitic grades, the duplex structure provides better resistance to chloride SCC. Actual performance in H2S service still depends on temperature, chloride level, betonen, and the applicable materials standard.
Erosionskorrosion
High material hardness combined with superior dynamic passive film regeneration helps the elbows withstand erosion-corrosion in services containing suspended solids, including some subsea slurry applications.
Lange Radius (LR) vs. Kurzer Radius (SR) Duplex-Bögen
The choice between Long Radius (R = 1,5D) und kurzer Radius (R = 1,0D) is normally based on pressure loss, flow conditions, Schweinchen, and available installation space.
Lange Radius (LR) ELLENBOGEN (R = 1,5D)
- Abstand von Mitte zu Ende: 1.5 mal dem Nennrohrdurchmesser (A = 1.5 × NPS).
- Reibungsbedingter Druckverlust: The larger bend radius generally produces a smoother change in direction and lower pressure loss.
- Molchfähigkeit: A common choice for lines that require conventional or intelligent pigging.
- Erosionsbeständigkeit: The larger radius can reduce local flow disturbance and may help limit erosion at the bend.
- Primäre Anwendungen: Überregionale Ölpipelines über große Entfernungen, Offshore-Unterwassersteigleitungen, Prozesschemikalienlinien.
Kurze Radien (SR) ELLENBOGEN (R = 1,0D)
- Abstand von Mitte zu Ende: Entspricht dem Nennrohrdurchmesser (A = 1.0 × NPS).
- Reibungsbedingter Druckverlust: Höherer Richtungsänderungswiderstand und leicht erhöhte Turbulenz.
- Molchfähigkeit: Less suitable where the piping system requires passage of rigid inspection pigs.
- Kompaktes Layout: Useful where the available layout space does not allow a long-radius elbow.
- Primäre Anwendungen: Unterwasser-Skid-Pakete, kompakte FPSO-Topside-Module, Maschinenräume von Schiffen, Kufensysteme.
ASME B16.9 90° langer Radius (LR) Ellenbogenabmessungen & Gewichtstabelle
Reference dimensions for ASTM A815 WPS UNS S32750 butt-weld 90-degree LR elbows (1/2″ bis 24″).
| Normale Größe (NPS) | Außendurchmesser (OD) [mm] | Mitte bis Ende (A) [mm] | Wandstärke (SCH10S) [mm] | Wandstärke (40er Jahre schief) [mm] | Wandstärke (Sch 80s) [mm] | ca.. Gewicht (40er Jahre schief) [kg] |
|---|---|---|---|---|---|---|
| 1/2″ (DN15) | 21.3 | 38.0 | 2.11 | 2.77 | 3.73 | 0.08 |
| 3/4″ (DN20) | 26.7 | 38.0 | 2.11 | 2.87 | 3.91 | 0.11 |
| 1″ (DN25) | 33.4 | 38.0 | 2.77 | 3.38 | 4.55 | 0.16 |
| 1-1/2″ (DN40) | 48.3 | 57.0 | 2.77 | 3.68 | 5.08 | 0.42 |
| 2″ (DN50) | 60.3 | 76.0 | 2.77 | 3.91 | 5.54 | 0.78 |
| 3″ (DN80) | 88.9 | 114.0 | 3.05 | 5.49 | 7.62 | 2.15 |
| 4″ (DN100) | 114.3 | 152.0 | 3.05 | 6.02 | 8.56 | 4.12 |
| 6″ (DN150) | 168.3 | 229.0 | 3.40 | 7.11 | 10.97 | 11.20 |
| 8″ (DN200) | 219.1 | 305.0 | 3.76 | 8.18 | 12.70 | 23.50 |
| 10″ (DN250) | 273.0 | 381.0 | 4.19 | 9.27 | 12.70 | 41.80 |
| 12″ (DN300) | 323.8 | 457.0 | 4.57 | 9.52 | 12.70 | 64.50 |
ASME B16.9 / MSS SP-43 90° kurzer Radius (SR) Ellenbogenabmessungen
Reference dimensions and weights for compact-radius Super Duplex 2507 Ellbogen (R = 1,0D).
| NPS-Größe | Außendurchmesser (OD) [mm] | Center-to-End-SR (A) [mm] | SCH 10S Wand [mm] | SCH 40S Wand [mm] | ca.. Gewicht (Sch 80s) [kg] |
|---|---|---|---|---|---|
| 1″ (DN25) | 33.4 | 25.4 | 2.77 | 3.38 | 0.14 |
| 1-1/2″ (DN40) | 48.3 | 38.1 | 2.77 | 3.68 | 0.35 |
| 2″ (DN50) | 60.3 | 50.8 | 2.77 | 3.91 | 0.65 |
| 3″ (DN80) | 88.9 | 76.2 | 3.05 | 5.49 | 1.80 |
| 4″ (DN100) | 114.3 | 101.6 | 3.05 | 6.02 | 3.40 |
| 6″ (DN150) | 168.3 | 152.4 | 3.40 | 7.11 | 9.80 |
| 8″ (DN200) | 219.1 | 203.2 | 3.76 | 8.18 | 19.50 |
Kritische Wärmebehandlung & Mikrostrukturelle Phasenbalance
The properties of ASTM A815 WPS UNS S32750 elbows depend on maintaining an appropriate 40%–60 % Ferrit / 60%–40 % Austenite Phasenverhältnis. Unsuitable heat treatment can promote intermetallic precipitation, including the embrittling Sigma-Phase (A) und Chi-Phase (H), which can reduce impact toughness and localized-corrosion resistance.
| Klasse / ASTM | Lösungsglühtemperatur | Kühlung / Abschreckmethode | Angestrebter Ferritgehalt |
|---|---|---|---|
| WPS S32750 (2507) | 1025°C – 1125°C [1920°F – 2060°F] | Schnelle Wasserlöschung (innerhalb von Sekunden unter 300°C) | 40% – 60% Ferrit (E562 Punkteanzahl) |
| WPS S31803 (2205) | 1020°C – 1100°C [1870°F – 2010°F] | Wasserabschreckung oder schnelle Luftkühlung | 40% – 60% Ferrit |
| WPS S32202 (2202) | 1020°C – 1080°C [1870°F – 1975°F] | Wasserabschreckung oder Zwangsluftabschreckung | 45% – 55% Ferrit |
Quench Rate: Cooling through the critical temperature range must be fast enough to limit intermetallic precipitation. The selected quench practice is intended to retain the required phase balance and mechanical properties.
Fertigungsabläufe für Seamless & Geschweißte Bögen
Typical production combines hot forming, hydraulic forming where applicable, end machining, Oberflächenbehandlung, and non-destructive examination.
Heiße Dornformung
For seamless fittings, the pipe or hollow stock is heated and formed over a mandrel so that the bend radius, wall distribution, and roundness stay within the required tolerances.
Plattenpressen & SCHWEIßEN
For larger fittings (>24″), plate may be formed into shells, prepared at the seams, and welded with a suitable super-duplex filler such as ER2594.
Volllösungsglühen
nach dem Formen, the elbows are solution annealed within the specified temperature range and rapidly cooled to restore the required phase balance.
Räumen & Oberflächenbeizen
The ends are machined to the required ASME B16.25 bevel geometry. Pickling and passivation are then used to remove heat tint and restore a clean passive surface.
Schweißspezifikation & Verbrauchsmaterialrichtlinien für S32750
Welding ASTM A815 WPS S32750 elbows requires controlled heat input and interpass temperature. Excessively rapid cooling can shift the HAZ phase balance, while excessive heat input or prolonged exposure can increase the risk of secondary phases.
| Schweißprozess | AWS-Füllmetallspezifikation | Empfohlene Wärmezufuhr | Abschirmung / Unterstützungsgas |
|---|---|---|---|
| GTAW (WIG) | AWS A5.9 ER2594 (Überlegiertes Ni ~ 9%) | 0.2 – 1.5 KJ/mm | Reines Ar oder Ar + 2% N2 / Ar + 30% Er + 2% N2 |
| SMAW (Stock) | AWS A5.4 E2594-16 / E2594-17 | 0.5 – 1.5 KJ/mm | N/A (Flussmittelbeschichtet) |
| GMAW (MICH) | AWS A5.9 ER2594-Draht | 0.5 – 1.2 KJ/mm | Ar + 2% N2 oder Ar + 30% Er + 2% N2 |
| SAH (Untergetauchter Bogen) | AWS A5.9 ER2594-Draht + Grundlegendes Flussmittel | 0.8 – 1.8 KJ/mm | Neutral / Grundlegendes Schweißpulver |
Die maximale Zwischenlagentemperatur muss strikt begrenzt werden 100° C (212° F) während aller Durchlaufsequenzen, um die Ausfällung von Sekundäraustenit und versprödenden Phasen zu verhindern.
Qualitätskontrolle & Testprotokolle
The inspection plan for ASTM A815 WPS UNS S32750 elbows normally combines material verification, Maßkontrollen, and the non-destructive or destructive tests specified by the purchase order and applicable standard.
1. PMI Testing
Positive Materialidentifizierung (PMI) by XRF or OES can be used to confirm the principal alloying elements and heat traceability.
2. Korrosionsprüfung
Where specified, ASTM G48 Method A testing can be used to evaluate resistance to ferric-chloride pitting and crevice corrosion.
3. Mikrostruktur & Ferrit
Metallographic examination, including ferrite measurement where required, is used to check phase balance and identify undesirable intermetallic phases.
4. radiologisch (RT) / OUT
Welded classes may require radiographic or ultrasonic examination according to the applicable specification, purchase order, and inspection plan.
internationale Standards & Äquivalente Bezeichnungsmatrix
| Standardorganisation | Standardcode | Beschreibung / Anpassungsart |
|---|---|---|
| ASTM-Standard | ASTM A815 / A815M | Standardspezifikation für geknetetes Ferrit, Ferritisch / austenitisch, und Rohrverbindungsstücke aus martensitischem Edelstahl |
| ASME-Standard | ASME B16.9 | Werksgefertigte Stumpfschweißbeschläge (NPS 1/2 durch NPS 48) |
| MSS-standard | MSS SP-43 | Geschmiedete und gefertigte Stumpfschweißfittings für Niederdruck, Korrosionsbeständige Anwendungen |
| MSS-standard | MSS SP-97 | Integral verstärkte geschmiedete Abzweig-Auslassanschlüsse – Muffenschweißen, Gewinde, und Stumpfschweißenden |
| Europäische Norm | De 10253-4 / De 10088-3 | Stumpfschweißen ROHR-FITTINGS – Knetaustenitisch und austenitisch-ferritisch (duplex) Rostfreier Stahl |
| NACE-Standard | Nace Mr0175 / ISO 15156 | Erdöl- und Erdgasindustrie – Materialien zur Verwendung in H2S-haltigen Umgebungen bei der Öl- und Gasförderung |
Wichtige industrielle Anwendungen für Super Duplex S32750-Bögen
Typical service areas include high-stress and corrosive industrial systems.
Offshore-Öl & Gasoberseiten
Used in subsea manifolds, Weihnachtsbäume, Stromlinien, Tragegurte, and firewater systems where seawater exposure and sour-service conditions place demanding requirements on corrosion resistance.
Meerwasserentsalzungsanlagen
Used in reverse-osmosis pump manifolds, brine headers, and energy-recovery systems handling concentrated saline water.
chemische Verarbeitung & Saure Pflanzen
Used in selected heat-exchanger, reboiler, and acid-service piping where the corrosion conditions exceed the practical limits of common austenitic grades.
Maßtoleranzen gemäß ASME B16.9 / MSS SP-43
| Nominale Rohr-Größe (NPS) | Abweichung vom Winkeltoleranz (Q) | Off-Plane-Toleranz (P) | Mitte-zu-Ende-Toleranz | Innendurchmesser am Ende |
|---|---|---|---|---|
| 1/2″ bis 2-1/2″ | ± 1 mm | ± 2 mm | ± 2.0 mm | +0.8 mm / -0.8 mm |
| 3″ bis 3-1/2″ | ± 2 mm | ± 3 mm | ± 2.0 mm | +1.6 mm / -1.6 mm |
| 4″ | ± 2 mm | ± 3 mm | ± 2.0 mm | +1.6 mm / -1.6 mm |
| 5″ bis 8″ | ± 3 mm | ± 5 mm | ± 2.0 mm | +1.6 mm / -1.6 mm |
| 10″ bis 18″ | ± 4 mm | ± 6 mm | ± 3.0 mm | +3.2 mm / -1.6 mm |
| 20″ bis 24″ | ± 5 mm | ± 10 mm | ± 3.0 mm | +4.8 mm / -1.6 mm |
Exportverpackung, Produktkennzeichnung & Qualitätszertifizierung
For export shipment, the fittings are protected against contamination, Feuchtigkeit, and handling damage, with identification marks retained for heat and product traceability.
Standardmarkierungsspezifikation
An jedem Ellbogen ist eine fortlaufende gestanzte Markierung angebracht: Herstellername/Logo, Standardcode (ASTM A815 WPS S32750), Rohr Größe, Wandstärke/Zeitplan, Laufzahl für 100% Rückverfolgbarkeit der Mühle.
Seetüchtige, begasungsfreie Holzkisten
Die Armaturen sind mit Endkappen aus Kunststoff geschützt, einzeln in feuchtigkeitsbeständiger Kunststofffolie verpackt, und in robuste, begasungsfreie Sperrholzkisten mit Stahlbandverstärkung verpackt.
De 10204 3.1 & 3.2 Mühlenzertifikate
Material Test Reports can be supplied to EN 10204 3.1, with third-party inspection available when required by the order.
Kurzreferenz zur Beschaffung
ASTM A815 WPS UNS S32750 Super Duplex Elbow-Datenkarte
Quick reference for engineering, procurement, and piping design work.
Sie müssen eingeloggt sein, um ein Kommentar abzugeben.