Technical Metrics & Material Attributes
Its yield strength is substantially higher than that of common austenitic grades such as 316L.
The higher proof stress can allow thinner wall schedules where the design calculation permits.
The PREN value is commonly used to assess resistance to localized pitting and crevice corrosion.
Commonly selected for sour service, offshore systems, and demanding chemical-service piping.
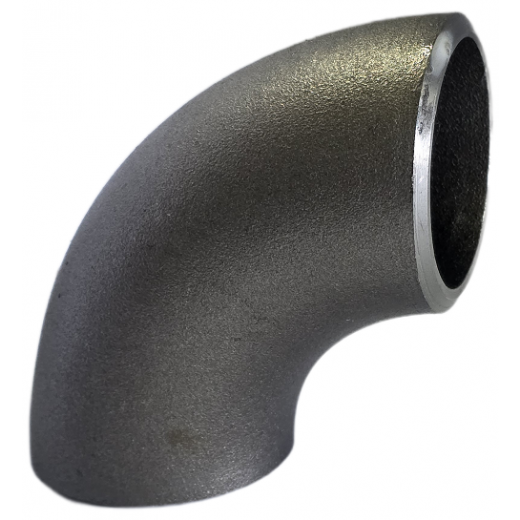
Material Overview: ASTM A815 WPS UNS S32750 Super Duplex Elbows
ASTM A815 WPS UNS S32750 is a wrought ferritic/austenitic super duplex stainless steel fitting grade used where strength and corrosion resistance are both important. It is used in marine, petrokimia, Subsea, and chemical-processing service where conventional stainless steels may not provide enough margin, AS S32750 (biasa dikenali sebagai 2507 Super Dupleks atau EN 1.4410) menawarkan yang seimbang 50/50 struktur mikro dwi fasa yang terdiri daripada perkadaran austenit dan ferit yang hampir sama. The duplex structure combines relatively high yield strength with good resistance to chloride-related stress corrosion cracking (SCC), while retaining useful toughness when the phase balance is properly controlled.
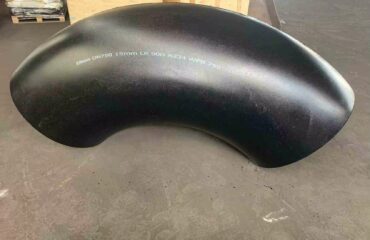
Penamaan WPS dalam ASTM A815 menunjukkan kelengkapan paip lancar gred tempa yang dihasilkan mengikut keperluan ASME B16.9 dan MSS SP-43 yang ketat. Siku ini, terdapat dalam kedua-duanya Panjang jejari (HOME, R = 1.5D) dan pendek Radius (SR, R=1.0 D) konfigurasi, are used to change flow direction in high-pressure piping networks. Sama ada digunakan dalam pelantar minyak luar pesisir laut dalam, loji penyahgaraman air laut osmosis songsang, penyental gas masam yang agresif, atau reaktor kimia ketulenan tinggi, ASTM A815 WPS UNS S32750 elbows are intended for service involving cyclic loading, temperature changes, and corrosive process fluids.
Klasifikasi Bahan Utama Dilindungi oleh Spesifikasi ASTM A815:
- Kelas WP-S: Kelengkapan lancar tempa yang dihasilkan daripada paip lancar, Tube, atau stok tempa.
- Kelas WP-W: Kelengkapan tempa yang mengandungi kimpalan di mana logam pengisi telah ditambah dan diperiksa tanpa merosakkan melalui radiografi (RT).
- Kelas WP-WX: Kelengkapan dikimpal tempa di mana semua kimpalan berada 100% diradiografi setiap ASME Boiler and Pressure Vessel Code.
- Kelas WP-WU: Kelengkapan tempa di mana semua kimpalan berada 100% diperiksa menggunakan ujian ultrasonik (OUT).
Had Komposisi Kimia (%) — UNS S32750 lwn Keluarga Dupleks
Elemental limits are controlled to support corrosion resistance and to reduce the risk of undesirable intermetallic phases such as sigma (a) and chi (h).
| Gred / UNS | Karbon (C) | Cr | Ni | Mo | N | Cu | MN (Max) | Si (Max) | P / S (Max) |
|---|---|---|---|---|---|---|---|---|---|
| WPS S32750 (2507) | ≤ 0.030 | 24.0 – 26.0 | 6.0 – 8.0 | 3.0 – 5.0 | 0.24 – 0.32 | ≤ 0.50 | 1.20 | 0.80 | 0.035 / 0.020 |
| WPS S31803 (2205) | ≤ 0.030 | 21.0 – 23.0 | 4.5 – 6.5 | 2.5 – 3.5 | 0.08 – 0.20 | - | 2.00 | 1.00 | 0.030 / 0.020 |
| WPS S32202 (2202) | ≤ 0.030 | 21.5 – 24.0 | 1.0 – 2.8 | 0.45 Max | 0.18 – 0.26 | - | 2.00 | 1.00 | 0.040 / 0.010 |
| WPS S32760 (sifar 100) | ≤ 0.030 | 24.0 – 26.0 | 6.0 – 8.0 | 3.0 – 4.0 | 0.20 – 0.30 | 0.50 – 1.00 | 1.00 | 1.00 | 0.030 / 0.010 |
* Nota: UNS S32750 mengandungi penambahan Nitrogen yang disengajakan (0.24–0.32%) untuk meningkatkan rintangan pitting dengan ketara, menggalakkan austenitisasi semula intergranular yang cepat semasa rawatan haba, dan meningkatkan kekuatan hasil mekanikal.
mekanikal & Data Prestasi Struktur
The ferrite-austenite balance gives S32750 high tensile and yield strength, useful low-temperature toughness, and good resistance to erosion-corrosion. Jika dibandingkan dengan standard 300 siri keluli tahan karat atau aloi dupleks tanpa lemak konvensional, S32750 membenarkan jurutera untuk menentukan jadual dinding yang lebih nipis (cth, SCH 10S lwn SCH 40S) tanpa mengorbankan margin keselamatan struktur.
Where permitted by the applicable ASME B31.3 design conditions, the higher allowable stress can reduce required wall thickness and system weight.
ASTM A815 S32750 Had Mekanikal
| Parameter Mekanikal | Had Piawai ASTM A815 |
|---|---|
| Kekuatan Tegangan, min (MPa / Ksi) | 800 – 965 / [116 – 140] |
| Menghasilkan Kekuatan (0.2% Offset), min | 550 MPa / [80 Ksi] |
| Pemanjangan dalam 2 dalam. (50 mm), min % | 15.0 % |
| Kekerasan, Brinell (HBW), Max | 310 HBW maks |
| Kekerasan, Rockwell C (HRC), Max | 32 HRC maks |
| Tenaga Kesan Charpy V-Notch (-40° C) | ≥ 80 Joule (rata-rata) |
Fizik Ketahanan Kakisan & Pengiraan Formula PREN
Pitting and crevice-corrosion resistance of Super Duplex UNS S32750 is commonly discussed using the Nombor setara rintangan pitting (KAYU). A higher PREN generally indicates greater resistance to localized passive-film breakdown in chloride-containing service.
mengadu & kakisan celah
Dengan sekurang-kurangnya PREN sebanyak 42, S32750 elbows are generally selected for chlorinated seawater service when the temperature and chloride exposure are within the design limits.
retak kakisan tegasan (SCC)
Compared with many austenitic grades, the duplex structure provides better resistance to chloride SCC. Actual performance in H2S service still depends on temperature, chloride level, tekanan, and the applicable materials standard.
Korosi hakisan
High material hardness combined with superior dynamic passive film regeneration helps the elbows withstand erosion-corrosion in services containing suspended solids, including some subsea slurry applications.
Panjang jejari (HOME) lwn Jejari Pendek (SR) Siku Dupleks
The choice between Long Radius (R = 1.5D) dan jejari pendek (R = 1.0D) is normally based on pressure loss, flow conditions, Babi, and available installation space.
Panjang jejari (HOME) SIKU (R = 1.5D)
- Jarak Pusat ke Hujung: 1.5 kali diameter paip nominal (A = 1.5 × NPS).
- Kehilangan Kepala Geseran: The larger bend radius generally produces a smoother change in direction and lower pressure loss.
- Keupayaan Pigging: A common choice for lines that require conventional or intelligent pigging.
- Rintangan Hakisan: The larger radius can reduce local flow disturbance and may help limit erosion at the bend.
- Aplikasi Utama: Saluran paip minyak merentas desa jarak jauh, anak naik dasar laut luar pesisir, memproses garis kimia.
pendek Radius (SR) SIKU (R = 1.0D)
- Jarak Pusat ke Hujung: Sama dengan diameter paip nominal (A = 1.0 × NPS).
- Kehilangan Kepala Geseran: Rintangan perubahan arah yang lebih tinggi dan pergolakan yang tinggi sedikit.
- Keupayaan Pigging: Less suitable where the piping system requires passage of rigid inspection pigs.
- Susun Atur Padat: Useful where the available layout space does not allow a long-radius elbow.
- Aplikasi Utama: Pakej gelincir dasar laut, modul bahagian atas FPSO padat, bilik enjin marin, sistem tergelincir.
ASME B16.9 Jejari Panjang 90° (HOME) Dimensi Siku & Carta Berat
Reference dimensions for ASTM A815 WPS UNS S32750 butt-weld 90-degree LR elbows (1/2″ dengan 24″).
| Saiz nominal (BOROUGH) | Diameter luar (OD) [mm] | Pusat untuk Akhir (A) [mm] | Ketebalan dinding (SCH 10S) [mm] | Ketebalan dinding (Skew 40s) [mm] | Ketebalan dinding (Sch 80s) [mm] | lebih kurang. Berat (Skew 40s) [kg] |
|---|---|---|---|---|---|---|
| 1/2″ (DN15) | 21.3 | 38.0 | 2.11 | 2.77 | 3.73 | 0.08 |
| 3/4″ (DN20) | 26.7 | 38.0 | 2.11 | 2.87 | 3.91 | 0.11 |
| 1″ (DN25) | 33.4 | 38.0 | 2.77 | 3.38 | 4.55 | 0.16 |
| 1-1/2″ (DN40) | 48.3 | 57.0 | 2.77 | 3.68 | 5.08 | 0.42 |
| 2″ (DN50) | 60.3 | 76.0 | 2.77 | 3.91 | 5.54 | 0.78 |
| 3″ (DN80) | 88.9 | 114.0 | 3.05 | 5.49 | 7.62 | 2.15 |
| 4″ (DN100) | 114.3 | 152.0 | 3.05 | 6.02 | 8.56 | 4.12 |
| 6″ (DN150) | 168.3 | 229.0 | 3.40 | 7.11 | 10.97 | 11.20 |
| 8″ (DN200) | 219.1 | 305.0 | 3.76 | 8.18 | 12.70 | 23.50 |
| 10″ (DN250) | 273.0 | 381.0 | 4.19 | 9.27 | 12.70 | 41.80 |
| 12″ (DN300) | 323.8 | 457.0 | 4.57 | 9.52 | 12.70 | 64.50 |
ASME B16.9 / MSS SP-43 90° Jejari Pendek (SR) Dimensi Siku
Reference dimensions and weights for compact-radius Super Duplex 2507 Siku (R = 1.0D).
| Saiz NPS | Diameter luar (OD) [mm] | SR Pusat ke Hujung (A) [mm] | Dinding SCH 10S [mm] | Dinding SCH 40S [mm] | lebih kurang. Berat (Sch 80s) [kg] |
|---|---|---|---|---|---|
| 1″ (DN25) | 33.4 | 25.4 | 2.77 | 3.38 | 0.14 |
| 1-1/2″ (DN40) | 48.3 | 38.1 | 2.77 | 3.68 | 0.35 |
| 2″ (DN50) | 60.3 | 50.8 | 2.77 | 3.91 | 0.65 |
| 3″ (DN80) | 88.9 | 76.2 | 3.05 | 5.49 | 1.80 |
| 4″ (DN100) | 114.3 | 101.6 | 3.05 | 6.02 | 3.40 |
| 6″ (DN150) | 168.3 | 152.4 | 3.40 | 7.11 | 9.80 |
| 8″ (DN200) | 219.1 | 203.2 | 3.76 | 8.18 | 19.50 |
Rawatan Haba Kritikal & Imbangan Fasa Mikro
The properties of ASTM A815 WPS UNS S32750 elbows depend on maintaining an appropriate 40%–60% ferit / 60%–40% Austenit nisbah fasa. Unsuitable heat treatment can promote intermetallic precipitation, including the embrittling Fasa Sigma (a) dan Fasa Chi (h), which can reduce impact toughness and localized-corrosion resistance.
| Gred / ASTM | Penyelesaian Penyepuh Suhu | Menyejukkan / Kaedah Pelindapkejutan | Kandungan Ferrite Sasaran |
|---|---|---|---|
| WPS S32750 (2507) | 1025°C – 1125°C [1920°F – 2060°F] | Pemadam Air Cepat (bawah 300°C dalam beberapa saat) | 40% – 60% Ferrite (E562 Kiraan Mata) |
| WPS S31803 (2205) | 1020°C – 1100°C [1870°F – 2010°F] | Water Quench atau Sejuk Udara Cepat | 40% – 60% Ferrite |
| WPS S32202 (2202) | 1020°C – 1080°C [1870°F – 1975°F] | Pemadam Air atau Pemadam Udara Paksa | 45% – 55% Ferrite |
Quench Rate: Cooling through the critical temperature range must be fast enough to limit intermetallic precipitation. The selected quench practice is intended to retain the required phase balance and mechanical properties.
Aliran Kerja Pembuatan untuk Lancar & Siku Dikimpal
Typical production combines hot forming, hydraulic forming where applicable, end machining, Rawatan permukaan, and non-destructive examination.
Pembentukan Mandrel Panas
For seamless fittings, the pipe or hollow stock is heated and formed over a mandrel so that the bend radius, wall distribution, and roundness stay within the required tolerances.
Penekan Plat & Welding
For larger fittings (>24″), plate may be formed into shells, prepared at the seams, and welded with a suitable super-duplex filler such as ER2594.
Penyepuhlindapan Penyelesaian Penuh
selepas terbentuk, the elbows are solution annealed within the specified temperature range and rapidly cooled to restore the required phase balance.
Beveling & Penjerukan Permukaan
The ends are machined to the required ASME B16.25 bevel geometry. Pickling and passivation are then used to remove heat tint and restore a clean passive surface.
Spesifikasi Kimpalan & Garis Panduan Bahan Habis untuk S32750
Welding ASTM A815 WPS S32750 elbows requires controlled heat input and interpass temperature. Excessively rapid cooling can shift the HAZ phase balance, while excessive heat input or prolonged exposure can increase the risk of secondary phases.
| proses kimpalan | Spesifikasi Logam Pengisi AWS | Input Haba yang Disyorkan | Perisai / Gas Penyokong |
|---|---|---|---|
| GTAW (TIG) | AWS A5.9 ER2594 (Terlebih aloi Ni ~ 9%) | 0.2 – 1.5 kJ/mm | Ar atau Ar tulen + 2% N2 / Ar + 30% Dia + 2% N2 |
| SMAW (tongkat) | AWS A5.4 E2594-16 / E2594-17 | 0.5 – 1.5 kJ/mm | n / a (bersalut fluks) |
| GMAW (SAYA) | Wayar AWS A5.9 ER2594 | 0.5 – 1.2 kJ/mm | Ar + 2% N2 atau Ar + 30% Dia + 2% N2 |
| MELIHAT (Arka Terendam) | Wayar AWS A5.9 ER2594 + Fluks Asas | 0.8 – 1.8 kJ/mm | Berkecuali / Fluks Kimpalan Asas |
Suhu interpass maksimum mestilah terhad kepada 100° C (212° F) semasa semua urutan laluan untuk mengelakkan pemendakan austenit sekunder dan fasa embrittling.
Kawalan kualiti & Protokol Pengujian
The inspection plan for ASTM A815 WPS UNS S32750 elbows normally combines material verification, semakan dimensi, and the non-destructive or destructive tests specified by the purchase order and applicable standard.
1. PMI Testing
Pengenalpastian bahan positif (PMI) by XRF or OES can be used to confirm the principal alloying elements and heat traceability.
2. Ujian Kakisan
Where specified, ASTM G48 Method A testing can be used to evaluate resistance to ferric-chloride pitting and crevice corrosion.
3. Struktur mikro & Ferrite
Metallographic examination, including ferrite measurement where required, is used to check phase balance and identify undesirable intermetallic phases.
4. Radiografi (RT) / OUT
Welded classes may require radiographic or ultrasonic examination according to the applicable specification, purchase order, and inspection plan.
piawaian antarabangsa & Matriks Jawatan Setara
| Organisasi Standard | Kod Standard | Penerangan / Jenis pemasangan |
|---|---|---|
| Piawaian ASTM | ASTM A815 / A815M | Spesifikasi Standard untuk Feritik Tempa, Ferit / austenit, dan kelengkapan paip keluli tahan karat martensit |
| Piawaian ASME | ASME B16.9 | Kelengkapan Buttweld Tempa Buatan Kilang (BOROUGH 1/2 melalui NPS 48) |
| standard MSS | MSS SP-43 | Kelengkapan Kimpalan Punggung Tempa dan Fabrikasi untuk Tekanan Rendah, Tahan Karat Aplikasi |
| standard MSS | MSS SP-97 | Kelengkapan Outlet Cawangan Tempa Diperkukuh Bersepadu — Kimpalan Soket, Thread, dan Buttweld Ends |
| Norma Eropah | EN 10253-4 / EN 10088-3 | kimpalan punggung KELENGKAPAN PAIP – Austenit tempa dan ferit austenit (Dupleks) Keluli Tahan Karat |
| Standard NACE | Nace Mr0175 / ISO 15156 | Industri petroleum dan gas asli — Bahan untuk digunakan dalam persekitaran yang mengandungi H2S dalam pengeluaran minyak dan gas |
Aplikasi Perindustrian Utama untuk Super Duplex S32750 Elbows
Typical service areas include high-stress and corrosive industrial systems.
Minyak Luar Pesisir & Bahagian Atas Gas
Used in subsea manifolds, pokok Krismas, garis alir, penaik, and firewater systems where seawater exposure and sour-service conditions place demanding requirements on corrosion resistance.
Tumbuhan Penyahgaraman Air Laut
Used in reverse-osmosis pump manifolds, brine headers, and energy-recovery systems handling concentrated saline water.
pemprosesan kimia & Tumbuhan Asid
Used in selected heat-exchanger, reboiler, and acid-service piping where the corrosion conditions exceed the practical limits of common austenitic grades.
Toleransi Dimensi setiap ASME B16.9 / MSS SP-43
| Nominal Paip Saiz (BOROUGH) | Toleransi Sudut Luar (Q) | Toleransi Luar Pesawat (P) | Toleransi Pusat ke Hujung | Diameter Dalam Di Hujung |
|---|---|---|---|---|
| 1/2″ kepada 2-1/2″ | ± 1 mm | ± 2 mm | ± 2.0 mm | +0.8 mm / -0.8 mm |
| 3″ kepada 3-1/2″ | ± 2 mm | ± 3 mm | ± 2.0 mm | +1.6 mm / -1.6 mm |
| 4″ | ± 2 mm | ± 3 mm | ± 2.0 mm | +1.6 mm / -1.6 mm |
| 5″ ke 8″ | ± 3 mm | ± 5 mm | ± 2.0 mm | +1.6 mm / -1.6 mm |
| 10″ ke 18″ | ± 4 mm | ± 6 mm | ± 3.0 mm | +3.2 mm / -1.6 mm |
| 20″ dengan 24″ | ± 5 mm | ± 10 mm | ± 3.0 mm | +4.8 mm / -1.6 mm |
Pembungkusan Eksport, Penandaan Produk & Pensijilan Kualiti
For export shipment, the fittings are protected against contamination, lembapan, and handling damage, with identification marks retained for heat and product traceability.
Spesifikasi Penandaan Standard
Tanda die-cop berterusan pada setiap siku termasuk: Nama/Logo Pengeluar, Kod Standard (ASTM A815 WPS S32750), Paip Saiz, Ketebalan Dinding/Jadual, Nombor Haba untuk 100% kebolehkesanan kilang.
Sarung Kayu Tanpa Pengasapan Layak Laut
Kelengkapan dilindungi dengan penutup plastik hujung, dibalut secara individu dalam filem plastik kalis lembapan, dan dibungkus ke dalam kotak papan lapis bebas pengasapan tugas berat dengan tetulang tali keluli.
EN 10204 3.1 & 3.2 Sijil Kilang
Material Test Reports can be supplied to EN 10204 3.1, with third-party inspection available when required by the order.
Rujukan Pantas Perolehan
Kad Data Siku Super Dupleks ASTM A815 WPS UNS S32750
Quick reference for engineering, procurement, and piping design work.


anda mesti log masuk untuk menghantar komen.